
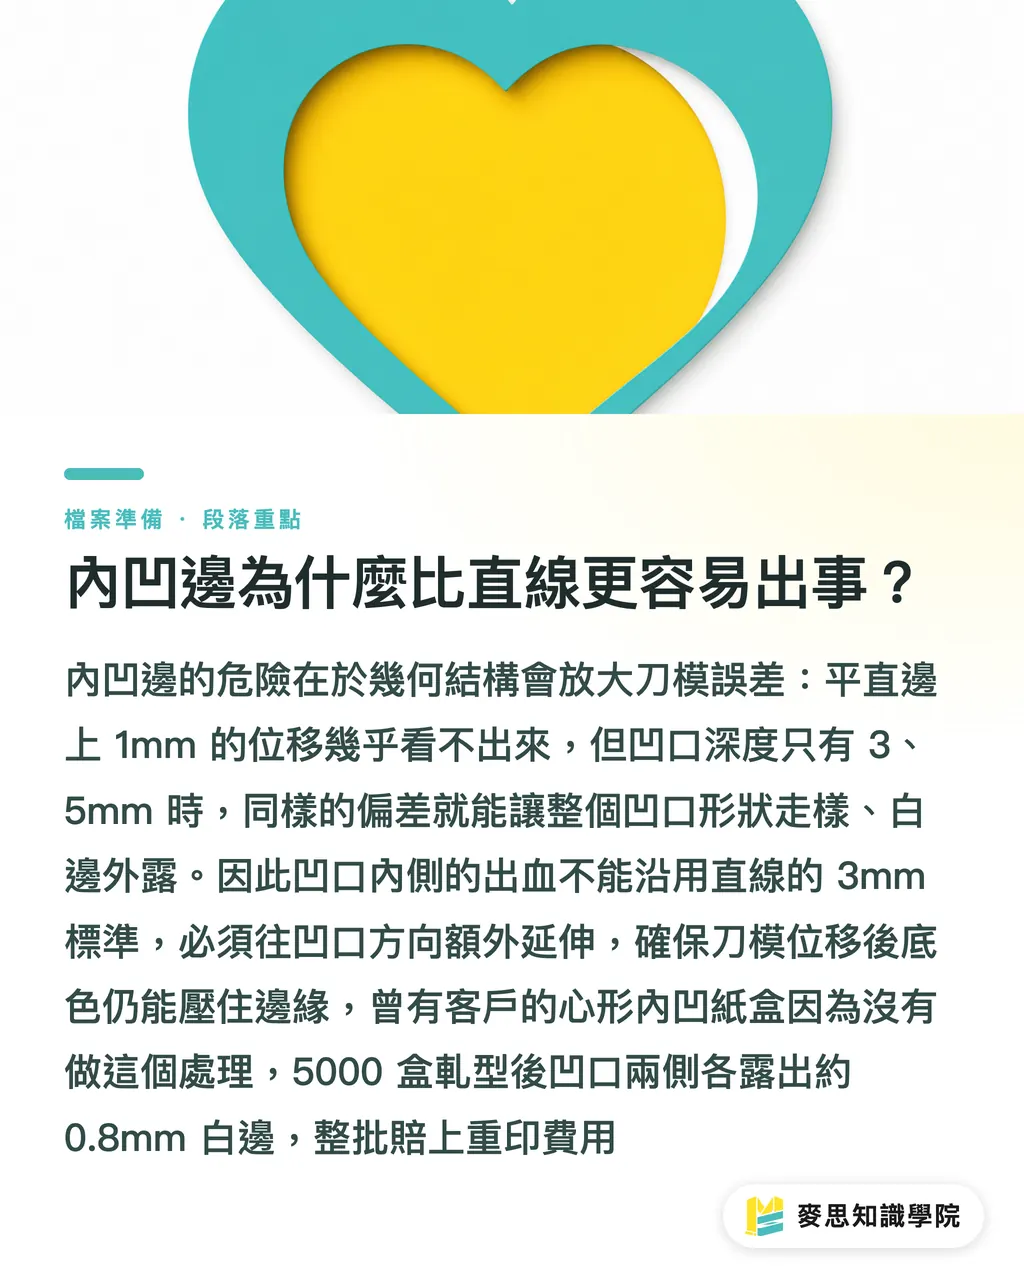
Why Do Inset Edges Fail More Easily Than Straight Edges?
Start with a basic idea: when die-cutting tolerance shows up on a straight edge, it usually just looks "slightly off." But on an inset edge, the same amount of deviation can shift the notch, expose a white edge, and in serious cases even cause the board to tear at the corner point
This is not exaggeration. It is a magnifying effect caused by structural geometry
In standard packaging printing, die-cutting registration tolerance is usually around ±0.5 to ±1mm by industry practice. Precision die cutters can hold tighter tolerances, but machine condition, board moisture content, and on-site temperature and humidity all affect the actual result. On a straight edge, this kind of tolerance is barely visible. But when an inset notch is only 3-5mm deep, a 1mm shift means the entire notch shape has changed
So bleed on inset edges cannot simply follow the same "3mm as a straight line" rule. Inside the notch, the bleed needs to keep extending toward the recessed direction, so even if the die shifts, the background color still covers the edge and no white shows. Protruding corner points follow the same logic. If the corner radius is too small, the stress concentration left by the cutting rule on the board can become the starting point for tearing during transport
The most typical failure I have seen was a batch of skincare boxes. The front panel had a heart-shaped inset for brand identity. In the final artwork, the area around the notch only had the standard 3mm bleed, with no extra extension into the recessed area. After die-cutting, about 0.8mm of white edge appeared on both sides of the notch. All 5000 boxes had to be reprinted and reprocessed
How Should Bleed Stop at Fold Lines?
The issue at fold lines is different from inset edges. It is often not "not enough bleed," but "bleed crossing the fold line and spilling onto another panel."
A paper box layout is a flat sheet before folding, but after folding, the graphics on each panel must align. If the background color or image bleed extends too far past the fold line, the edge of the neighboring panel may show a color that should not be there, forming a color band along the box edge. It looks cheap
In practice, the bleed on each side of a fold line only needs to extend up to the fold line. In other words, the bleed line should not cross the fold line. Some factories stop it 1mm before the fold line. That is more conservative and suits board materials with lower folding precision, such as board with a high recycled pulp ratio or larger thickness tolerance
One detail often missed: important text, Logos, and barcodes should keep at least 4-5mm of safety distance from fold lines. After folding, the board on both sides of the crease shifts slightly because of paper thickness. The industry calls this paper thickness compensation. On thick board above 350g, this shift can reach 1-1.5mm. Put the brand name right against the fold line, and it will look crooked after folding
When MINDS handles custom packaging, it recalculates folding compensation for each board thickness. This is worth confirming clearly with the printer before placing the order
How Should Join Areas, Glue Tabs, and Tuck-In Tabs Be Sized?
Paper box joins generally fall into two types: glue tabs, fixed with adhesive, and tuck-in tabs, which interlock without glue. These two place very different demands on final artwork
A standard glue tab is usually 10-15mm wide. This gives the glue nozzle on an automatic folder-gluer enough working surface:
・Too narrow, under 8mm: the machine can easily apply glue off-position, causing the seam to open
・Too wide: it wastes material. If the folded glue tab presses against the printed artwork, it also affects appearance
・Printing on the glue-tab side: leaving it blank is recommended, or printing only a light background. Heavy dark solids and varnish both reduce adhesion between glue and paper fibers, making the join more likely to open after some use
Tuck-in structures depend more heavily on board stiffness and thickness. There is no universal size. If the locking length of the tuck-in tab is much shorter than the height of the side panel, the tab will feel loose. If it is too long, insertion resistance can become so high that the board gets damaged. A common starting point is to set the tuck-in locking depth at around one-third of the box height, but board gsm, structure shape, and opening frequency all have to be considered
Another detail often missed: the outer edges of glue tabs and tuck-in tabs also need bleed extension, usually the standard 3mm. Otherwise, after die-cutting, that edge becomes a white line, clearly visible along the outside of the assembled box
How Do Hot Stamping and Coating Affect Die Structure Safety?
Post-press finishing is the layer of packaging die safety most easily overlooked at the final-artwork stage
Hot stamping takes place under localized heat and pressure, usually around 80-120°C. This process locally heats the board and slightly changes local dimensions. If the hot-stamped area sits too close to a fold line, under 3mm, the crease depth along that section can become uneven after heat pressing, making irregular folded corners more likely
I once handled a tea gift box project with full hot stamping across the front face. The stamped edge was only 2mm from the top fold line. After stamping, the crease along that section had almost disappeared. When the lid was folded, the board chose its own "path of least resistance" along the stamping edge, leaving an obvious irregular slanted corner on the lid. We redesigned the stamping boundary and moved it back 4mm. Problem solved
Spot UV needs the same attention. Varnish film has thickness. If the edge of a spot UV area lands right on a fold line, the transition between thick and thin layers becomes a visible raised line after folding, especially under certain lighting angles
Practical rules:
・Keep hot stamping and spot UV boundaries at least 3mm away from fold lines
・Keep them at least 2mm away from die-cut trim lines. This refers to the design boundary, not the bleed line itself
・If the glue-tab surface has been coated, tell the vendor in advance so they can switch to a suitable adhesive formula
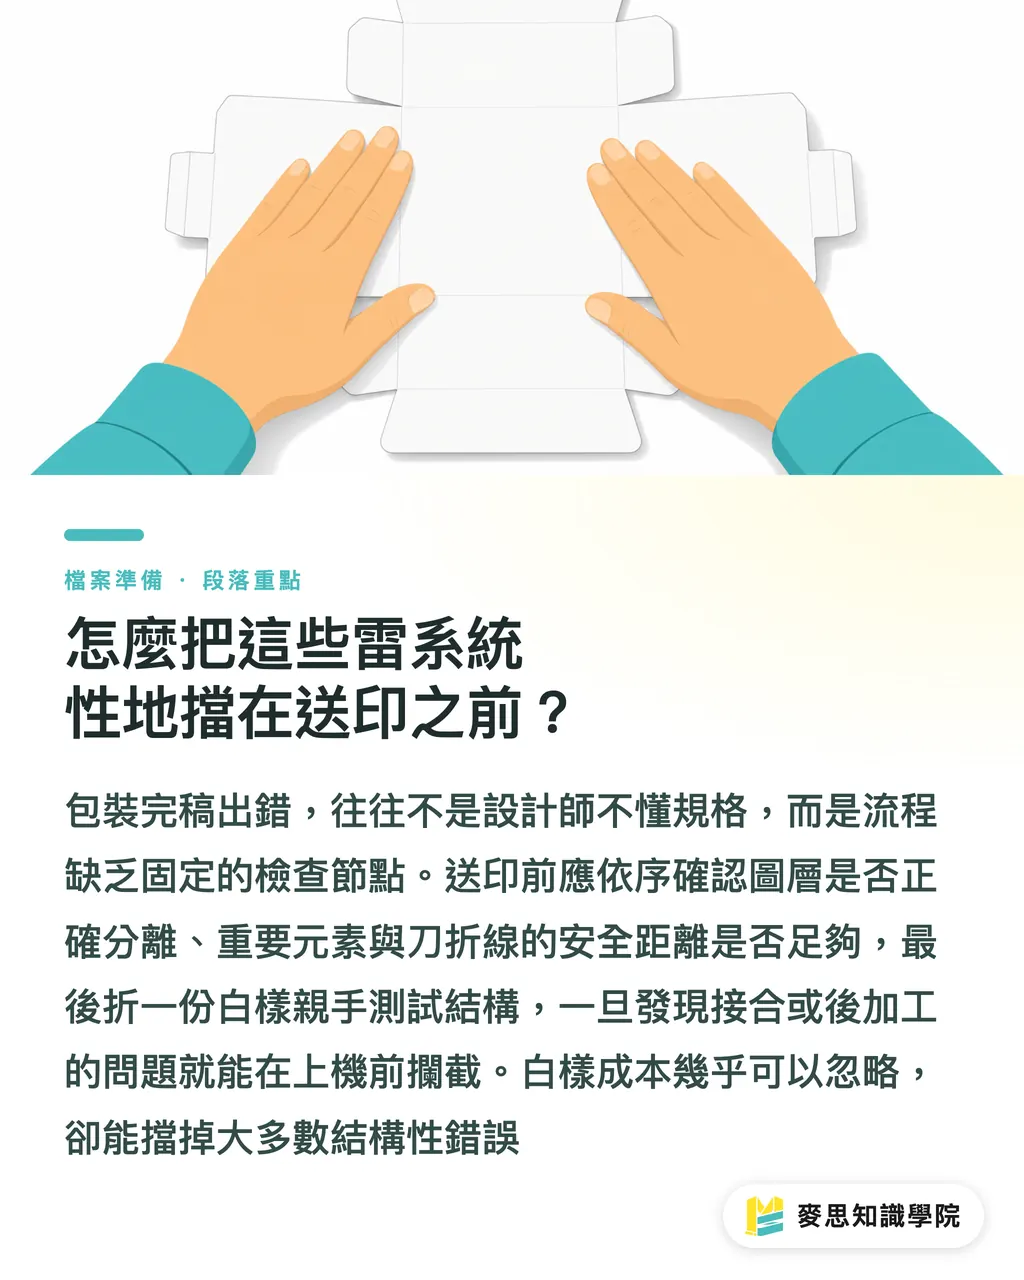
How Do You Catch These Problems Before Sending Files to Print?
Most of the problems above do not happen because designers lack knowledge. They happen because the final-artwork workflow does not make die safety distance a fixed checkpoint. The three-gate prepress thinking used by MINDS (MS, mid-to-high-end fully custom commercial printing) can be applied directly to packaging final artwork:
・Gate 1: Layer separation check: die lines, fold lines, bleed lines, and safety lines are each placed on independent layers with clear names, not mixed into the print artwork
・Gate 2: Position and safety-distance self-check: all important elements, text, Logos, barcodes, and post-press finishing boundaries, are at least 4mm from fold lines and at least 3mm from trim lines. Bleed on inset edges extends further into the notch direction. The glue-tab surface is checked to confirm there is no dark printing or varnish
・Gate 3: Physical mockup check: before running a complex structural box on press, make a white mockup, either blank die-cutting or digital output. Fold it, tuck it, and glue it once to check whether the join is firm, the fold lines are clean, and the finishing boundaries are safe
The cost of making a white mockup is almost negligible, but it can block most structural problems. When a designer folds and glues it by hand once, they learn faster than by reading any specification manual
If you are not sure whether your final-artwork specs are qualified, you can consult the Mai Strategy Knowledge Academy consulting team before sending files to print and run one structural die check
Key Takeaways
・Bleed on inset edges cannot be copied from the straight-line standard. The inside of the notch needs extra extension toward the recessed direction, because die-cutting tolerance has a geometric magnifying effect on notch shape
・Bleed on both sides of a fold line should stop at the fold line. Bleed crossing the fold line is a common final-artwork mistake, and after folding, the edge may show a color that should not be there
・Important text and Logos should stay at least 4mm away from fold lines. On thick board above 350g, add paper thickness compensation as well, or the visual shift after folding will be obvious
・Avoid dark printing or coating on glue-tab surfaces. Adhesive strength drops on both ink layers and varnish layers, making the join more likely to open after use
・Hot stamping and spot UV boundaries should stay at least 3mm away from fold lines. Otherwise, post-press heat pressure or film thickness difference can throw the crease out of spec
Further Thoughts
Packaging final-artwork problems almost all share one trait: the designer is looking at a flat dieline, but the actual acceptance target is a three-dimensional structure. This gap in viewpoint is especially obvious around inset edges, fold-line boundaries, and join areas. The real poka-yoke method is not sticking a spec sheet on the wall. It is building safety-distance checks into the workflow, and ideally making physical white mockup confirmation a standard step instead of an optional one to skip. If your project has complex inset shapes, hot stamping, spot UV, or similar post-press finishing, add one more structural die check before printing. Time spent up front is far cheaper than rejected shipments and reprints after delivery
FAQ
- How much bleed is enough for inset edges on paper packaging boxes?
- Inset edges should not use only the standard 3mm. The inside of the notch needs bleed to continue extending along the recessed direction, making sure no white edge appears even if the die shifts within ±1mm. The shallower the notch and the higher the allowed shift ratio, the more generous the bleed needs to be
- How far should a Logo or text sit from a fold line at minimum?
- At least 4mm. For thick board above 350g, 5mm is recommended, because after the board is folded, the two panels shift due to paper thickness, known as paper thickness compensation. If important elements sit too close to the fold line, they will look visually biased to one side after folding
- Why should the glue-tab surface avoid dark printing or full-area varnish?
- The glue tab is the adhesive bonding surface. Ink layers, especially dark solids, and varnish films both block direct contact between the adhesive and the paper fibers. This lowers bonding strength and makes the join more likely to open after some use. Leaving the glue tab blank is recommended, or printing only a light background color
- What specific problems happen when hot stamping is too close to a fold line?
- Hot stamping is done under high temperature, 80-120°C, and high pressure. After the board is locally heated, both the depth and position of the crease may be affected. After folding, irregular folded corners can appear, known in the industry as a weak or false fold. The hot-stamping boundary should stay at least 3mm away from the fold line
- Is there a simple way to self-check whether final artwork for a complex structural box is safe?
- Making a white mockup is the most direct method. Cut one sheet of white card with the die, then actually fold, tuck, and glue it once. This checks fold-line accuracy, join strength, and whether the post-press finishing boundaries are safe. The cost is almost negligible, and it can catch most structural problems
Related articles

The Print × AI weekly
The print and AI know-how designers, brands and enterprises can use before they commit — one email, every week
MINDS Free Tools
Imposition calculator and preflight file check — free prepress tools, right in your browser.
MINDS Group
Need actual printing or gifting services?
From premium printing to online ordering and festive gifts — the MINDS Group sister brands take it from here.